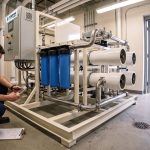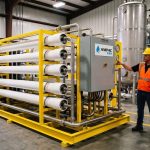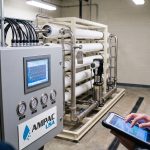
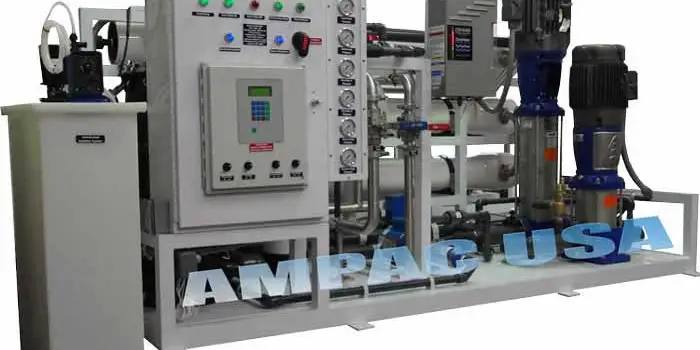

AMPAC USA won a contract from Fluor Construction to deliver two industrial reverse osmosis water purification plants to the Oyu Tolgoi gold and copper mining project. This mine is deep in Mongolia’s Gobi Desert. Each unit makes 80,000 gallons of pure, fresh drinking water every day (that’s 12.7 m³/hr). This water supports a workforce of 40,000 employees living right there on site. Why? Because there’s no natural fresh water supply in that whole region. This project really shows how you can build water independence on an industrial scale, even in one of the world’s toughest, most isolated places.
- Client: Oyu Tolgoi Gold and Copper Mine, Gobi Desert, Mongolia (through Fluor Construction)
- Systems supplied: Two industrial reverse osmosis plants
- Capacity: 80,000 GPD (12.7 m³/hr) each, so 160,000 GPD total
- People served: 40,000 employees living on site, rotating every 3 months
- Source water: Brackish groundwater from Gobi Desert aquifers
- AMPAC USA: We’re ISO 9001:2015 certified, and we’ve put systems in 40+ countries since 1994
The Water Problem at Oyu Tolgoi: Mining in the Gobi Desert
The Oyu Tolgoi mine, in Mongolia’s South Gobi Desert, holds one of the biggest gold and copper deposits ever found. It’s such a huge project that it attracted investment from Rio Tinto and the Mongolian government. Fluor Corporation, one of the world’s largest engineering and construction companies, stepped in to manage its development.
But the Gobi Desert is one of the toughest places on Earth for a lot of people to live. It gets less than 200 millimeters of rain a year. There’s basically no surface water for hundreds of kilometers between the mine and the closest towns. The groundwater you do find under the Gobi? It’s mostly brackish, meaning it’s packed with dissolved salts, minerals, and in some spots, arsenic and fluoride. These levels are way higher than what the WHO says is safe for drinking water.
A mining camp housing 40,000 employees, who live there for three-month shifts, needs roughly 2–4 million gallons of drinking water every day for everything. That includes drinking, cooking, sanitation, medical facilities, fire suppression, and even keeping dust down on roads and processing areas. The only real solution was industrial-scale water purification. They needed technology that could turn that brackish groundwater into water meeting WHO drinking standards. And it had to be reliable, because 40,000 people’s daily survival depended on it.
Why They Chose Industrial Reverse Osmosis
Fluor Construction looked at a lot of different water supply technologies for Oyu Tolgoi before they picked reverse osmosis. What were they looking for? The system needed to handle brackish groundwater with varying and potentially high TDS. It had to be proven reliable in remote places with little maintenance help. It needed to scale up for different phases of camp growth, have a modular design for easy installation in the desert without special construction gear, and offer a good operating cost per cubic meter of water produced.
Reverse osmosis was the clear winner. Unlike thermal desalination, which needs a lot of heat energy (tough to supply efficiently in a remote spot), RO systems run on electricity. The mine’s on-site power infrastructure could handle that. And unlike chemical treatment, RO makes water that meets drinking standards even when the source water chemistry changes. That’s a huge plus when you’re dealing with desert aquifers that can vary a lot across the extraction area.
AMPAC USA was chosen to supply two industrial RO plants for the project. Each unit produces 80,000 GPD (gallons per day), which is about 12.7 cubic meters per hour, or 302 cubic meters daily. Together, these two units make 160,000 GPD, roughly 600 cubic meters of drinking water every day. That was enough to supply the initial camp population before they added more capacity later.
Technical Specs: Industrial RO for Desert Mining
The industrial reverse osmosis plants we sent to Oyu Tolgoi were built specifically for the Gobi Desert’s harsh conditions. Standard commercial RO systems, made for mild climates and treated city water, would quickly fail there. AMPAC USA designed these systems from the ground up to handle the unique challenges of this location.
What Was in the Source Water
Gobi Desert groundwater is tough stuff to treat. Total dissolved solids (TDS) in desert aquifer water usually range from 1,000 to 5,000 mg/L, or even higher. That’s classified as brackish water. The specific mix of ions includes high levels of sulfates, chlorides, and in some Mongolian aquifer zones, fluoride and arsenic. These need extra treatment steps beyond standard RO. Before we designed the system, AMPAC USA did a full water quality analysis. We looked at TDS, pH, hardness, alkalinity, sulfate, chloride, nitrate, iron, manganese, silica, arsenic, and fluoride to make sure our pre-treatment was right and the final water met WHO standards for everything.
Pre-Treatment System
The pre-treatment for the Oyu Tolgoi systems protected the RO membranes from the high fouling potential of desert groundwater. It included multi-media depth filtration to remove suspended solids and fine particles. We added activated carbon adsorption to get rid of organic compounds and oxidizing agents that could hurt the membrane polymer. There were also anti-scalant chemical dosing systems to stop minerals from building up at higher concentrations, and in-line cartridge filtration as a final guard right before the high-pressure pump.
High-Pressure RO Membrane Stage
The AMPAC USA industrial reverse osmosis systems use brackish water RO membranes that run at 150–300 psi (10–21 bar). That’s perfect for the TDS range of Gobi aquifer water. Each 80,000 GPD unit has multiple pressure vessels arranged side-by-side, and each vessel holds 6–7 spiral-wound membrane elements. The system gets a recovery rate of 70–75%. That means 70–75% of the source water becomes product water, and only 25–30% is discharged as concentrated brine. We optimized this recovery rate for the available groundwater and the need to manage brine disposal in a desert.
Desert-Specific Design Features
Running a water purification system in the Gobi Desert needs design choices you just don’t think about in mild, developed areas:
- Extreme temperature tolerance: Gobi Desert temperatures swing from -40°C in winter to +40°C in summer. We designed the systems with insulation, heat tracing for exposed pipes and membrane elements, and cooling features to keep them at the right operating temperature all year.
- Sand and dust protection: Mining operations kick up a lot of airborne particles. These would quickly clog open electrical and mechanical parts. All enclosures are rated IP65 or higher, and air intakes for electrical panels use coarse filters to keep out fine sand.
- Simple maintenance: There aren’t special water treatment technicians on site, and the closest major repair shop is hundreds of kilometers away. So, we designed the systems for camp maintenance crews with basic mechanical skills to operate and do routine upkeep.
- Spare parts: AMPAC USA sent a full initial inventory of spare parts, enough for 24 months of operation. This let the mine keep the systems running without relying on supply chains for everyday consumables.
- Modular transport and installation: We designed the systems to fit in standard shipping containers. They could be installed without heavy construction equipment, using the mine’s own vehicle fleet for lifting and placement.
The Scale of the Challenge: Water for 40,000 People in the Desert
Forty thousand people living on site, with a full workforce always present, is like a small city. Meeting their water needs in a place with no natural fresh water is a huge engineering task. It demands industrial-grade reliability and backup systems.
Here’s a typical breakdown of water use for a big mining camp:
- Drinking water: At least 4–5 liters per person per day; the WHO recommends 10 liters for good hydration in hot, physically demanding work.
- Food prep and cooking: 3–5 liters per person per day.
- Personal hygiene (handwashing, bathing): 15–30 liters per person per day.
- Medical and sanitation: 50–100 liters per person per day in well-equipped camp medical facilities.
- Laundry: 10–15 liters per person per day for washing clothes and linens.
The WHO suggests a minimum of 50 liters per person per day for all personal and household uses in temporary settlements. For 40,000 workers, that’s at least 2 million liters (about 530,000 gallons) of drinking quality water every day just for personal use and hygiene. And that doesn’t even count water for industrial processes, dust suppression, or fire protection systems.
Industrial Water Treatment for Mining and Resource Extraction
The Oyu Tolgoi project is a great example of a problem mining operations everywhere face: getting safe water to huge, remote workforces when natural fresh water isn’t there or isn’t enough. Global Water Intelligence says the mining sector used about 9–10 billion cubic meters of water globally in recent years. That’s more than several medium-sized countries use in an entire year.
Water management at mines increasingly involves a full cycle of treating, reusing, and recycling water. AMPAC USA’s industrial water treatment systems help with many parts of this cycle:
- Feed water purification: Converting brackish groundwater, river water, or process water to potable or process-grade quality
- Process water treatment: Providing specific water quality parameters for mineral processing, flotation, and hydrometallurgical operations
- Produced water treatment: Processing mine drainage, tailings pond water, and acid mine drainage (AMD) for reuse or safe discharge
- Zero liquid discharge (ZLD): Treating brine concentrate to minimize or eliminate liquid discharge in environmentally sensitive desert environments
AMPAC USA Capabilities in Remote Industrial Water Supply
AMPAC USA has been supplying industrial water treatment systems to remote and demanding environments since 1994. Our systems have been deployed in deserts, Arctic environments, remote Pacific islands, offshore oil platforms, and military forward operating bases — wherever reliable, high-quality water production is needed far from municipal supply infrastructure.
All AMPAC USA systems are manufactured under ISO 9001:2015 quality management systems and are designed to NSF/ANSI 58 standards where drinking water applications require certification. Our engineering team provides comprehensive project support from initial water quality analysis through system design, factory testing, delivery, commissioning, and long-term service support.
For large-scale industrial water supply projects, AMPAC USA works directly with EPC contractors like Fluor Corporation, as well as with mine owners, government agencies, and development finance institutions. Our experience with international logistics, remote installation, and multi-year service contracts makes us a reliable partner for projects in any location on earth.
Explore our industrial water treatment capabilities, learn about our brackish water treatment systems, or visit our water treatment systems page for specifications. To discuss a remote or industrial water supply project, contact our engineering team. Read more about AMPAC USA’s history and global deployments on our company page, or explore more project case studies on our blog.
Step-by-Step: How AMPAC USA Approaches Remote Industrial Water Projects
- Water quality analysis: Comprehensive testing of all available water sources — groundwater, surface water, recycled process water — to characterize feed water chemistry and identify contaminants requiring treatment.
- Process design: Selection of pre-treatment, primary treatment (RO, NF, UF), post-treatment, and disinfection stages based on feed water characteristics and product water requirements.
- System sizing: Capacity calculation based on population, consumption standards, storage requirements, and production schedule, including redundancy factor for maintenance periods.
- Engineering and documentation: Complete P&ID, equipment datasheets, civil/structural requirements, electrical single-line diagrams, and instrumentation diagrams for integration with site construction plans.
- Manufacturing and factory acceptance testing: Systems are manufactured in AMPAC USA’s production facility, fully assembled and tested against water quality specifications before shipment.
- Logistics and installation support: AMPAC USA coordinates shipping to remote sites, provides installation supervision, and commissions systems to operational readiness.
- Training and handover: Site personnel receive comprehensive training on operation, routine maintenance, and troubleshooting before AMPAC USA’s commissioning team demobilizes.
- Ongoing service support: Remote diagnostics, planned maintenance visits, and spare parts programs maintain system performance through the project’s operational life.
Frequently Asked Questions: Industrial RO Water Treatment for Mining and Remote Sites
What type of water purification systems did AMPAC USA supply to the Oyu Tolgoi mine?
AMPAC USA supplied two industrial reverse osmosis (RO) water purification plants to the Oyu Tolgoi gold and copper mining project. These systems were specifically designed to convert the available brackish groundwater into pure fresh drinking water for the onsite workforce.
What was the combined daily water production capacity of AMPAC USA’s systems at Oyu Tolgoi?
The two industrial reverse osmosis plants supplied by AMPAC USA to the Oyu Tolgoi mine had a combined daily production capacity of 160,000 gallons per day (GPD). Each unit was engineered to produce 80,000 GPD (12.7 m³/hr) of potable water.
What were the primary water challenges at the Oyu Tolgoi mine in Mongolia’s Gobi Desert?
The Oyu Tolgoi mine faced extreme water scarcity in the Gobi Desert, with annual rainfall less than 200 millimeters and no viable surface water. The existing groundwater was predominantly brackish, high in dissolved salts, minerals, and in some aquifers, arsenic and fluoride concentrations exceeding WHO safe drinking water guidelines.
How many employees did AMPAC USA’s water purification systems serve at the Oyu Tolgoi mine?
AMPAC USA’s industrial reverse osmosis plants were designed to provide pure fresh drinking water for a workforce of 40,000 employees living onsite at the Oyu Tolgoi gold and copper mining project. These systems supported daily survival needs for personnel residing in three-month rotations.
What makes the Oyu Tolgoi project a significant demonstration of industrial water independence?
The Oyu Tolgoi project demonstrates industrial-scale water independence by converting highly brackish groundwater into potable water for 40,000 people in one of the world’s most extreme and remote desert environments. AMPAC USA’s ISO 9001:2015 certified expertise ensured a reliable water supply where natural sources were unsuitable or non-existent.
Related Articles
- RO Water Quality: What TDS, pH, and Conductivity Actually Mean for Your System
- NSF/ANSI 58 RO System Certification: What It Covers and What It Doesn't
- Reverse Osmosis System Maintenance Guide: Service Intervals and Procedures
- RO Rejection Rate: What It Means, How to Measure It, and What Decline Signals | AMPAC USA
Conclusion
Two 80,000 GPD plants turning brackish Gobi Desert groundwater into WHO-standard drinking water for 40,000 people is a good illustration of what industrial RO can do when there’s simply no other water source to fall back on. The engineering that made it work — extreme-temperature tolerance, IP65-rated enclosures against sand and dust, and a 24-month spare parts inventory — is the same playbook we apply to any remote or industrial site with no municipal supply nearby. If your operation faces a similar water-scarcity problem, explore our industrial water treatment systems or contact our engineering team at info@ampac1.com or (909) 548-4900 to discuss your project.
AMPAC USA engineers custom water purification systems for commercial, industrial, and emergency applications — from 500 GPD to multi-million GPD. Trusted by municipalities, military, and industry worldwide.